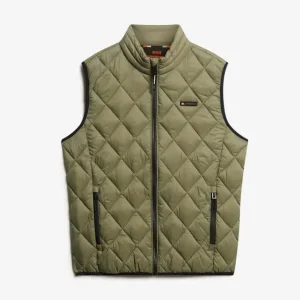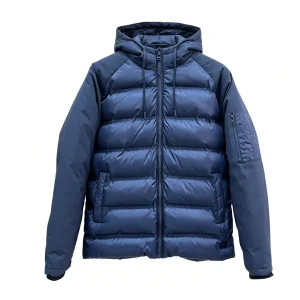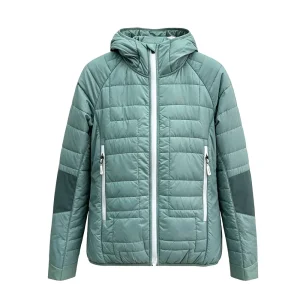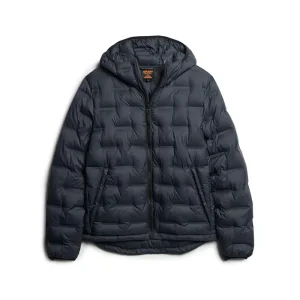
Engineered to deliver high color fastness, seam protection, and advanced thermal retention across dynamic corporate and consumer usage environments.
Why Quanzhou's industrial cluster drives sustainable, cost-optimized, and hyper-reliable global apparel manufacturing.
In modern performance and everyday circular-knit manufacturing, simple assembly has been replaced by end-to-end material engineering. As a core category underpinning every major apparel catalog, famous T-shirt products demand strict adherence to dimensional stability, colorfastness under continuous laundering, and sustainable fiber sourcing. ZanQian Garment Co., Ltd., based in the high-density textile hub of Quanzhou Taiwanese Investment Zone, Fujian, leverages decades of cluster proximity to revolutionize how brands develop, source, and scale apparel programs.
The strategic advantage of China's performance manufacturing ecosystem is centered on immediate localized raw material supply chains. Within a 30-kilometer radius, knitting mills, OEKO-TEX standard dye houses, automated screen-printing centers, and trim specialists collaborate via shared MES (Manufacturing Execution Systems). This proximity compresses cycle time: prototype turns occur within 3 to 5 business days, compared to the 3-week delays typical of distributed supply chains across Southeast Asia.
Furthermore, digitalized warehouse control, in-house tensile and hydrostatic testing laboratories, and six streamlined lean production lines allow ZanQian to maintain an overall qualified product acceptance threshold exceeding 98%. Enterprise buyers avoid downstream recall exposure through systematic raw-yarn inspection, intermediate seam shear testing, and finished garment inspections according to standard Acceptable Quality Limits (AQL 1.5/2.5).
Understanding shifting consumer values, strict environmental governance, and tech-driven production paradigms.
Global brands demand GRS-certified (Global Recycled Standard) recycled polyester, organic GOTS cotton blends, and closed-loop cellulose fibers. Lowering Scope 3 emissions has evolved from a marketing differentiator into a non-negotiable vendor onboarding requirement.
Modern B2B buyers integrate digital CLO 3D rendering to eliminate redundant physical prototyping stages. Digital twins accelerate fit approval, reducing sampling textile waste by up to 68% and cutting pre-production timelines by weeks.
The boundary separating active outdoor apparel and lifestyle apparel has dissolved. Today's famous T-shirt and technical collections integrate moisture-wicking capillary channels, silver-ion antibacterial protection, and UPF50+ ultraviolet shielding.
Navigating strict tariff policies, labor welfare audits, and environmental trade regulations with full transparency.
ZanQian facilities operate under certified SMETA and BSCI social audit standards, verifying safe working environments, clean ventilation systems, fire protocols, and fair wage structures for 150+ skilled garment workers.
Strict European REACH regulations and US CPSIA guidelines demand complete elimination of harmful AZO dyes, heavy metals, formaldehyde, and perfluorinated chemicals (PFAS-free finishing), fully certified via testing labs.
Our multilingual merchandising team coordinates directly with client sourcing departments. Proximity to Xiamen and Quanzhou ports ensures rapid sea and air transit, with automated customs documentation and DDP/FOB versatility.
From tactical uniforms to high-end lifestyle fashion, our products deliver consistent functional outcomes.
Custom uniform solutions engineered for logistics operators, aviation ground support, and hospitality networks requiring anti-pilling longevity (Martindale abrasion > 25,000 revs) and consistent corporate color reproduction across repeat bulk batches.
Ultralight running, mountaineering base layers, and outdoor trekking tees engineered with flatlock anti-chafing seams, ergonomic raglan gussets, and hydrophilic moisture dispersion for immediate body heat regulation.
Tailored oversized silhouettes, vintage enzyme washes, dense heavyweight single jerseys (240–320 GSM), and high-density silicone or puff screen prints developed directly from client mood boards to premium retail rack execution.
Essential operational details to simplify supply chain decision-making for corporate apparel buyers.
Our standard production MOQs range from 500 to 1,000 pieces per style and colorway, depending on custom yarn dye specifications and fabric weight. For in-stock performance textile formulations, lower initial pilot trial volumes can be supported.
We deploy computerized Datacolor spectrophotometer analysis matching lab dips to Delta E < 0.8 standards. All dyed lots undergo multi-wash tests, crocking assessments (wet/dry), and artificial light-exposure verification before roll batch cutting.
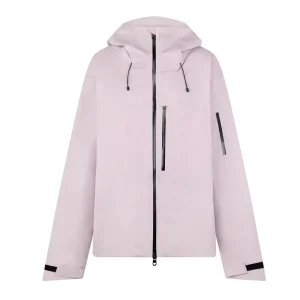
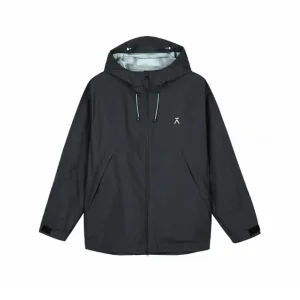
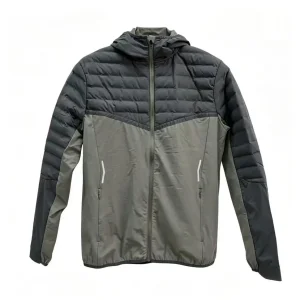
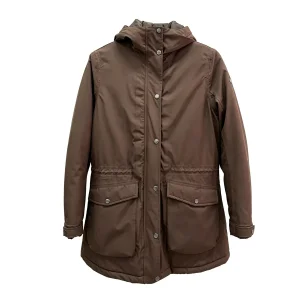
Yes. Our facility specializes in technical outerwear, heated garments, and seamless heat-pressed lamination. Our R&D team translates client tech packs into structural CAD pattern markers while validating seal integrity under pressure washing.
Proto sampling requires 7 to 10 days upon tech pack receipt. Following final Golden Sample sign-off and lab dip approval, full commercial production completes in 35 to 50 days, depending on textile intricacy and seasonal slot capacity.
High-performance outerwear designed to complement base layer T-shirts and corporate technical uniform programs.